Ask a workshop how long a repair takes and the answer is usually the wrench time — "two hours." Ask the machine and the answer is the elapsed time — three days, most of it spent waiting for a seal kit, a free technician, or a supervisor to say yes. That gap between wrench time and elapsed time is where fleets lose availability, and it is almost entirely made of waiting that nobody measures because nobody can see it. This page breaks a work order's clock into its segments, names the three bottlenecks that stretch it, and shows the live board that cuts it in half — sign up free and start the clock on your next work order tonight.
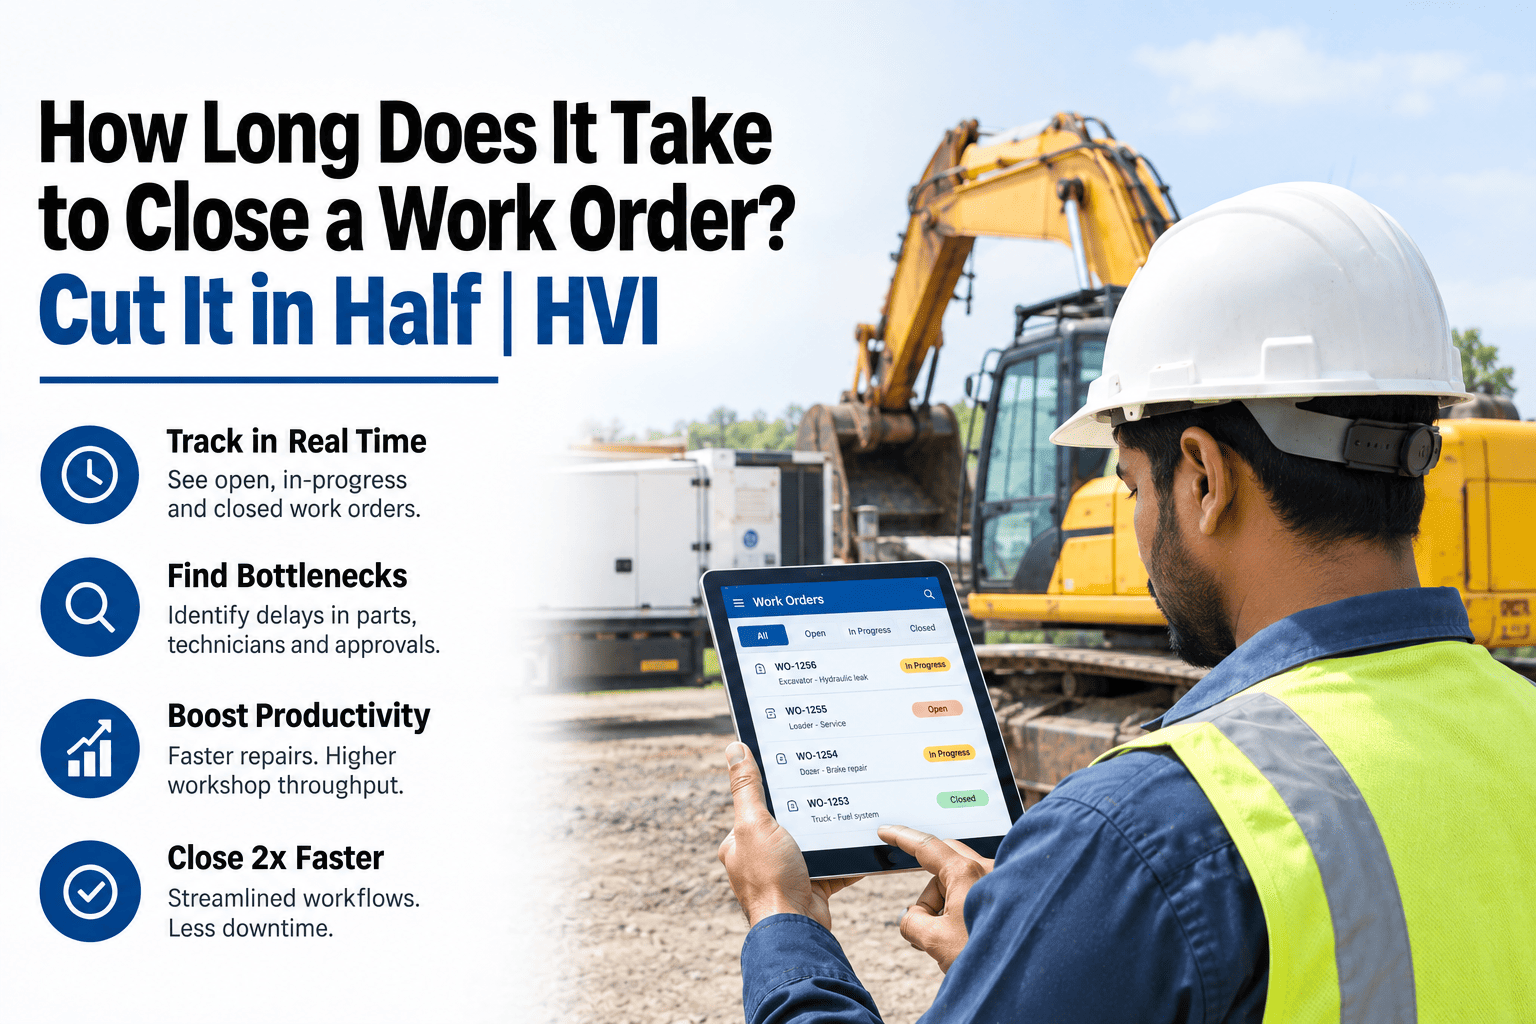
How Long Does It Take to Close a Work Order? Cut It in Half
Track every work order live from raised to closed, see exactly where the hours go — parts, technicians, approvals — and remove the waiting that stands between a two-hour repair and a three-day one.
Where a Three-Day Work Order Actually Goes
Raised to Assigned
The request sits in a chat or on a sheet until a planner happens to see it and gives it an owner — often overnight, sometimes days for a non-critical item, and occasionally never, because a message to a group of thirty-eight people is a request to nobody in particular. The machine keeps working with the defect in it for the whole of this segment, and the clock has already started even though nobody is watching it yet.
Assigned to Started
The technician has it on a list but is on another machine, or the job waits for the excavator to be free of production, or both — and because the list is ranked by who asked loudest rather than by severity and age, a brake fault and a cracked mirror wait in the same queue. On paper this segment does not exist; the job card starts when the work starts, and the day and a half before it never gets counted.
Waiting for Parts
The machine is opened, the seal kit is not on the shelf, and the job stops — the technician moves to another machine, a purchase order goes out, and the excavator sits half-dismantled for two days waiting on a part that could have been reserved when the job was assigned. This is the single largest segment in most Indian workshops and the most invisible, because nothing on a paper job card records the day the work paused.
Wrench Time
The actual repair — the two hours of hands on the machine that the workshop quotes when asked how long the job takes, and the only segment anyone was ever measuring. The mechanics are usually competent and usually quick; the myth that repairs are slow because technicians are slow survives only because every other segment of the clock was hidden from view.
Closure and Approval
Waiting for a supervisor's sign-off, a test run, or an approval on a cost that exceeded somebody's limit — the machine is repaired but not released, which to the production team is exactly the same as not repaired. A fixed excavator standing in the bay overnight because the person with the signature went home at six is downtime by another name, and it is the easiest segment on the whole clock to remove.
Shares are indicative patterns, not fixed figures — but the shape is what matters: wrench time is a fraction of the clock, and everything else is waiting. Cutting the cycle in half never means faster mechanics; it means shorter waits.
The Three Bottlenecks, and Their Signals
The Job Opened Before the Part Arrived
Signal: jobs sitting in "waiting for parts." Fix: parts reserved at assignment, and no bay time booked until the kit is on the shelf.
Assigned but Not Started
Signal: the gap between assignment and first hour logged. Fix: a queue ranked by severity and age, with load visible per technician.
Repaired but Not Released
Signal: repaired machines sitting unreleased. Fix: self-release thresholds, phone sign-off at the machine, and an aging alert.
Put a Clock on Every Work Order This Week
Every work order carries its timestamps from raised to released, the live board shows what is waiting and why, and the cycle-time report breaks the clock into its segments by machine, technician, and site — configured for your workshop in an afternoon. Bring last month's job cards to a 30-minute session and our India team shows where your hours went.
The Live Board the Whole Workshop Works From
Every card carries its time in each column, so the board is also the report — the site manager sees at a glance whether this week's hours are stuck in Waiting or spread across Assigned, and the fix goes to the column that is full.
Before and After, Segment by Segment
Raised to Assigned
Assigned to Started
Waiting for Parts
Wrench Time
Closure and Release
Total Elapsed
Indicative durations for routine repairs on a mid-size fleet — your segments vary, which is exactly why the report measures them per workshop instead of assuming them.
Five Moves That Halve the Cycle
Timestamp Every Transition
Raised, assigned, started, waiting, closed, released — each change of status stamped automatically, so the cycle-time report exists before anyone has to build it and the first week's numbers show where the hours actually go.
Reserve Parts at Assignment, Not at the Bay
The planner reserves the kit when the job is assigned, the storekeeper stages it, and the technician opens the machine with the part in hand — the single move that removes the largest segment from most workshops' clocks.
Rank the Queue, Show the Load
Jobs order themselves by severity and age, technician load is visible per person, and the planner books work into production windows — so "assigned" means a real slot, not a place in a mental list.
Make Waiting Visible and Named
A job cannot sit in Waiting without a reason — part, machine, or approval — and each reason has an owner and an age, so the daily stand-up reads the Waiting column instead of guessing why the bay is empty.
Release From the Machine
The supervisor signs off on the phone at the machine, routine jobs below a cost threshold release themselves, and a repaired machine that sits unreleased past a set number of hours raises an alert — because a fixed machine that production cannot use is still downtime.
Frequently Asked Questions
What is a good work order cycle time for a construction fleet?
It depends on severity — critical faults measured in hours, routine repairs commonly within a day, and planned services inside their booked window. The useful number is your own trend by segment, which is why the report measures each workshop rather than quoting a universal target.
Our parts wait is a supplier problem, not a workshop one. Does this help?
It shows which parts stall jobs most often and for how long, so reorder points move to the right items and the supplier conversation is about specific part numbers and days lost rather than a general complaint — most fleets find a short list of items causes most of the waiting.
Will technicians resist having their time tracked?
Less than expected — the report shows most of the delay was never theirs, and a technician whose queue is ranked and whose parts are staged spends less of the day hunting and more of it fixing. The tracking usually vindicates the workshop.
Does the live board work at remote sites with no signal?
Yes — status changes, hours, and photos record on the device and sync when coverage returns with their original timestamps, so the cycle-time report is accurate even for the bench that has never had a bar of signal; sign up free and test it in airplane mode.
Can we see our own cycle time before committing?
Bring a month of job cards or a week of your repair chat to a session — our India team rebuilds them as timestamped work orders and shows the segment breakdown for your workshop. Book the 30-minute demo and bring the busiest month.
The Mechanics Were Never the Problem. The Waiting Was.
A two-hour repair that takes three days is not a slow workshop — it is an invisible queue, an unstaged part, and an unsigned release, and all three shrink the moment they are measured. Start free and put a clock on every work order this week, or bring your job cards to a 30-minute session and see where your hours go.